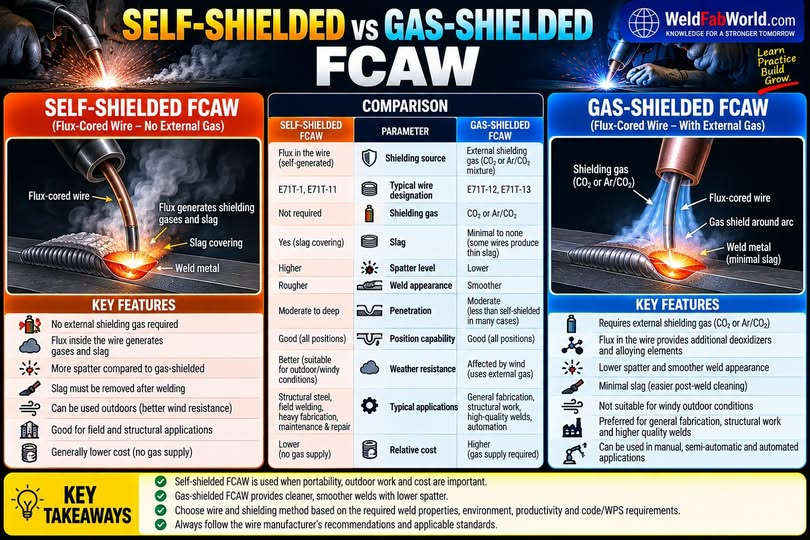
Both use a flux-cored wire, but the shielding method is different.
• SELF-SHIELDED FCAW (FCAW-S)
The flux inside the wire generates the shielding gases and slag.
√ No external shielding gas
√ Excellent for field/outdoor welding
√ More tolerant of windy conditions
√ Good portability
» More fumes/spatter can occur
» Slag must be removed between passes
• GAS-SHIELDED FCAW (FCAW-G)
Uses flux-cored wire plus external shielding gas, commonly CO₂ or Ar/CO₂ mixtures depending on the wire classification.
√ Smooth arc and good weld appearance
√ Generally lower spatter
√ High productivity
√ Excellent for controlled fabrication environments
» External gas supply required
» Shielding can be disrupted by wind
♦ Easy memory:
FCAW-S → Flux creates shielding
FCAW-G → Flux + external gas
♦ Important: Select the wire and shielding method according to the wire classification, manufacturer recommendations, WPS and applicable code/specification.
Post time: Oct-08-2026