Choosing the correct SMAW electrode isn’t simply about matching the stainless-steel grade. You also need to consider chemical composition, service temperature, corrosion environment, mechanical properties, dissimilar-metal welding and the qualified WPS.
♦ COMMON ELECTRODE SELECTIONS
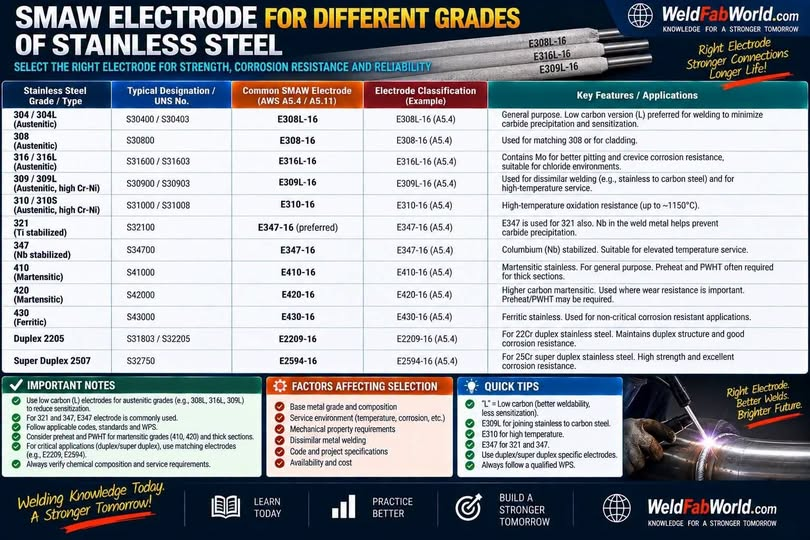
Stainless Steel Typical SMAW Electrode 304 / 304L,E308L-16,308,E308-16,E316 / 316L,E316L-16,E309 / 309L,E309L-16,E310 / 310S,E310-16,E321,347/E347-16,E410/E410-16E,420/E420-16,E430E/430-16,Duplex 2205/E2209-16,Super Duplex 2507/E2594-16.
♦ WHY DOES ELECTRODE SELECTION MATTER?
• 304L → E308L
Low-carbon weld metal helps reduce sensitization concerns.
• 316L → E316L
The filler contains Mo to support the required corrosion performance.
• 321 / 347 → E347
E347 weld metal is commonly selected because its Nb stabilization is suitable for these applications.
• Carbon Steel → Stainless Steel
E309L is commonly used for many stainless-to-carbon-steel joints, subject to the design and WPS.
• Duplex → E2209
Designed specifically for duplex 2205 applications and intended to support appropriate weld-metal properties.
• Super Duplex → E2594
Used for matching super-duplex applications where the specified properties and corrosion resistance are required.
※ IMPORTANT: These are common examples, not universal rules. Always verify the exact electrode classification against the material specification, project specification, applicable code and qualified WPS.
» Easy memory trick:
304 → 308L
316 → 316L
309 → Dissimilar welding
310 → High temperature
321/347 → 347
2205 → 2209
2507 → 2594
Post time: Oct-28-2026