

1. Description & Applications
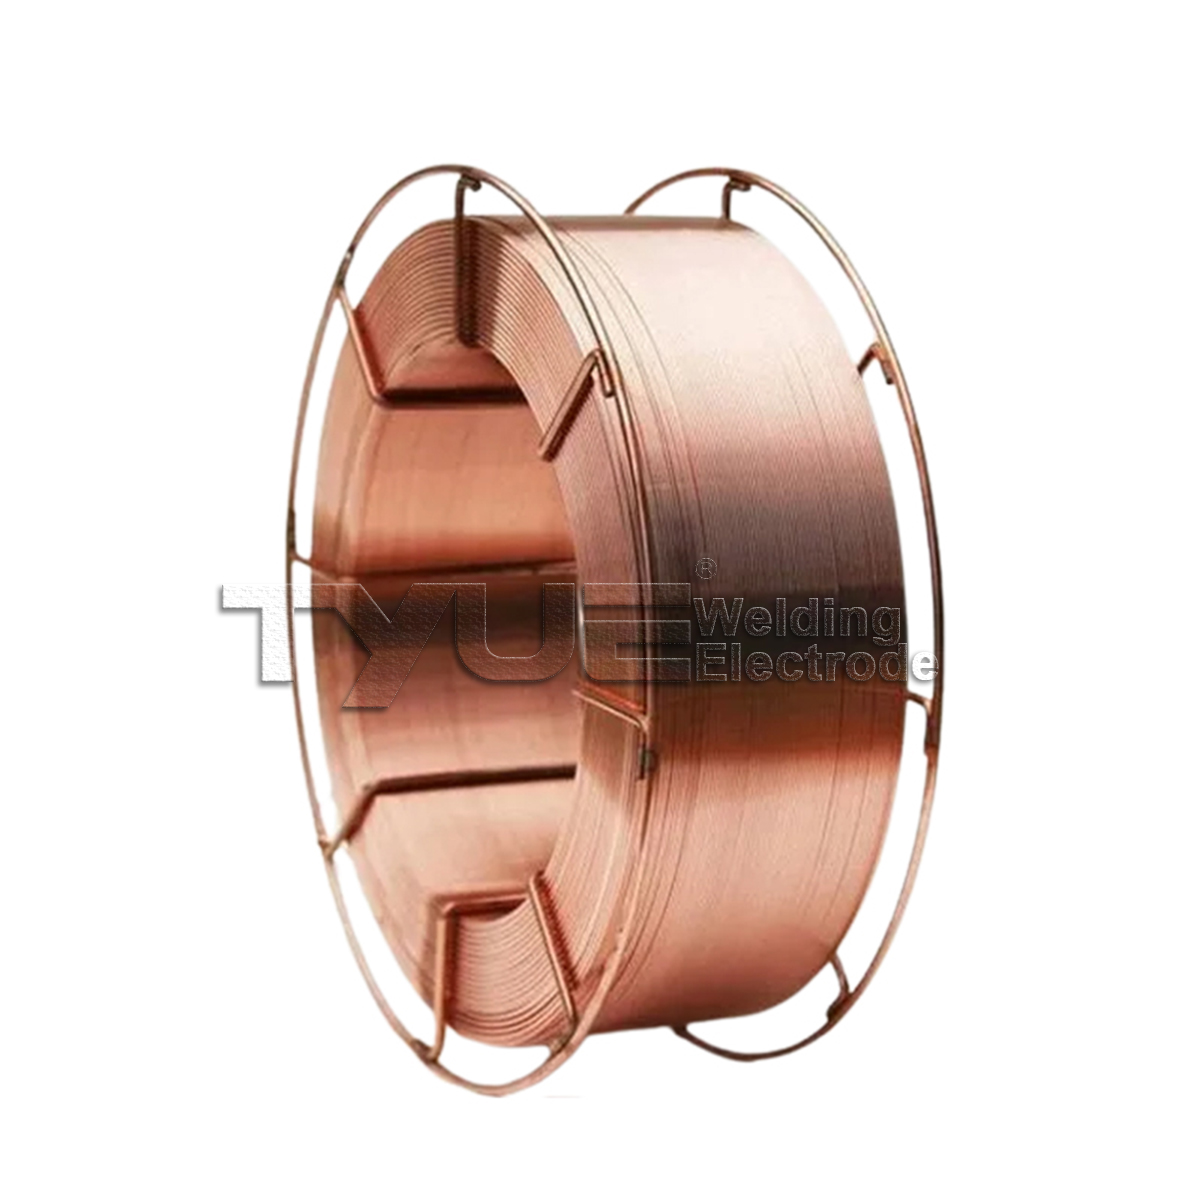
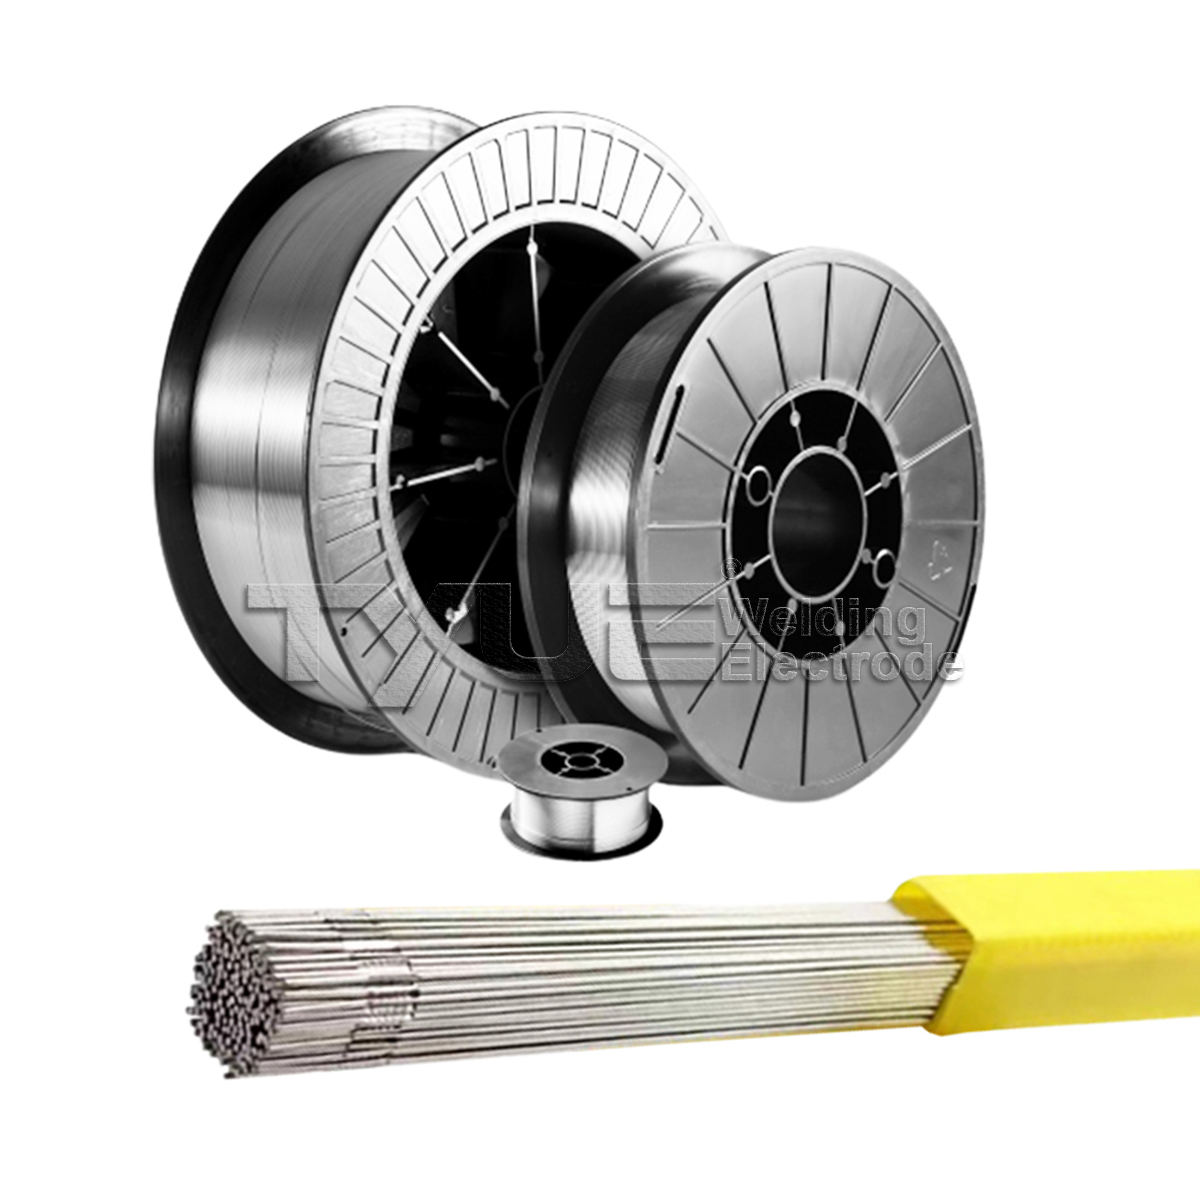
ER385 (commonly referred to as 904L filler metal) is a fully austenitic solid stainless steel wire used for welding matching high-alloy materials. With high levels of Chromium, Nickel, Molybdenum, and an addition of Copper, ER385 provides exceptional resistance to general corrosion, pitting, crevice corrosion, and stress corrosion cracking in aggressive environments, particularly in sulfuric, phosphoric, and organic acid media.
Key Applications:
- Base Metals: Designed for joining matching alloy 904L (UNS N08904, W.Nr. 1.4539), Uranus B6, and similar high-alloy austenitic steels. Also suitable for dissimilar joins between 904L and standard austenitic grades (e.g., 316L, 317L).
- Corrosion Resistance: Outstanding resistance to reducing environments, sulfuric acid across a wide concentration range, wet-process phosphoric acid, and high-chloride marine/brackish water environments.
- Industries: Flue gas desulfurization (FGD) systems, chemical and petrochemical processing, seawater cooling systems, paper and pulp bleaching units, fertilizer production, and pickling equipment.
2. Classification & International Standards
CLASSIFICATION: AWS A5.9 / ASME SFA 5.9 ER385
EQUIVALENT STANDARDS: EN ISO 14343-A: W 20 25 5 Cu L (TIG) / G 20 25 5 Cu L (MIG) | W.Nr. / DIN 1.4519 / 1.4539
UNS NUMBER: UNS N08904
3. Chemical Composition (wt. %)
| Element | Carbon (C) | Silicon (Si) | Manganese (Mn) | Chromium (Cr) | Nickel (Ni) | Molybdenum (Mo) | Copper (Cu) | Phosphorus (P) | Sulfur (S) |
| Min. | - | - | 1.00 | 19.50 | 24.00 | 4.20 | 1.20 | - | - |
| Max. | 0.025 | 0.50 | 2.50 | 21.50 | 26.00 | 5.20 | 2.00 | 0.020 | 0.010 |

4. Typical Mechanical Properties (As-Welded)
| Condition | Tensile Strength (Rm) | Yield Strength (Rp0.2) | Elongation (A5) | Hardness |
| As-Welded | ≥ 930 MPa(135,000 psi) | ≥ 750 MPa(108,000 psi) | 8%-12% | ~30-35HRC |
| H900 (PWHT: 480ºC/1 hr) | ≥ 1310 MPa(190,000 psi) | ≥ 1,170 MPa(170,000 psi) | 10%-14% | ~30-35HRC |
| H1150 (PWHT: 620ºC/4 hr) | ≥ 960 MPa(140,000 psi) | ≥ 720 MPa(105,000 psi) | 14%-18% | ~30-35HRC |
5. Storage & Handling Notes
- Store wire in a dry environment, protected from moisture; use promptly after opening or reseal properly.
- Clean the base metal surface before welding to remove oil, grease, and moisture.
- Preheating is generally not required (unless specified by the base material); post-weld heat treatment is usually not required. Under special conditions, solution annealing (approximately 1070-1100°C) followed by water quenching may be performed .
- Ensure adequate ventilation during welding, as welding fume contains chromium, nickel, and other constituents.