

1. Description
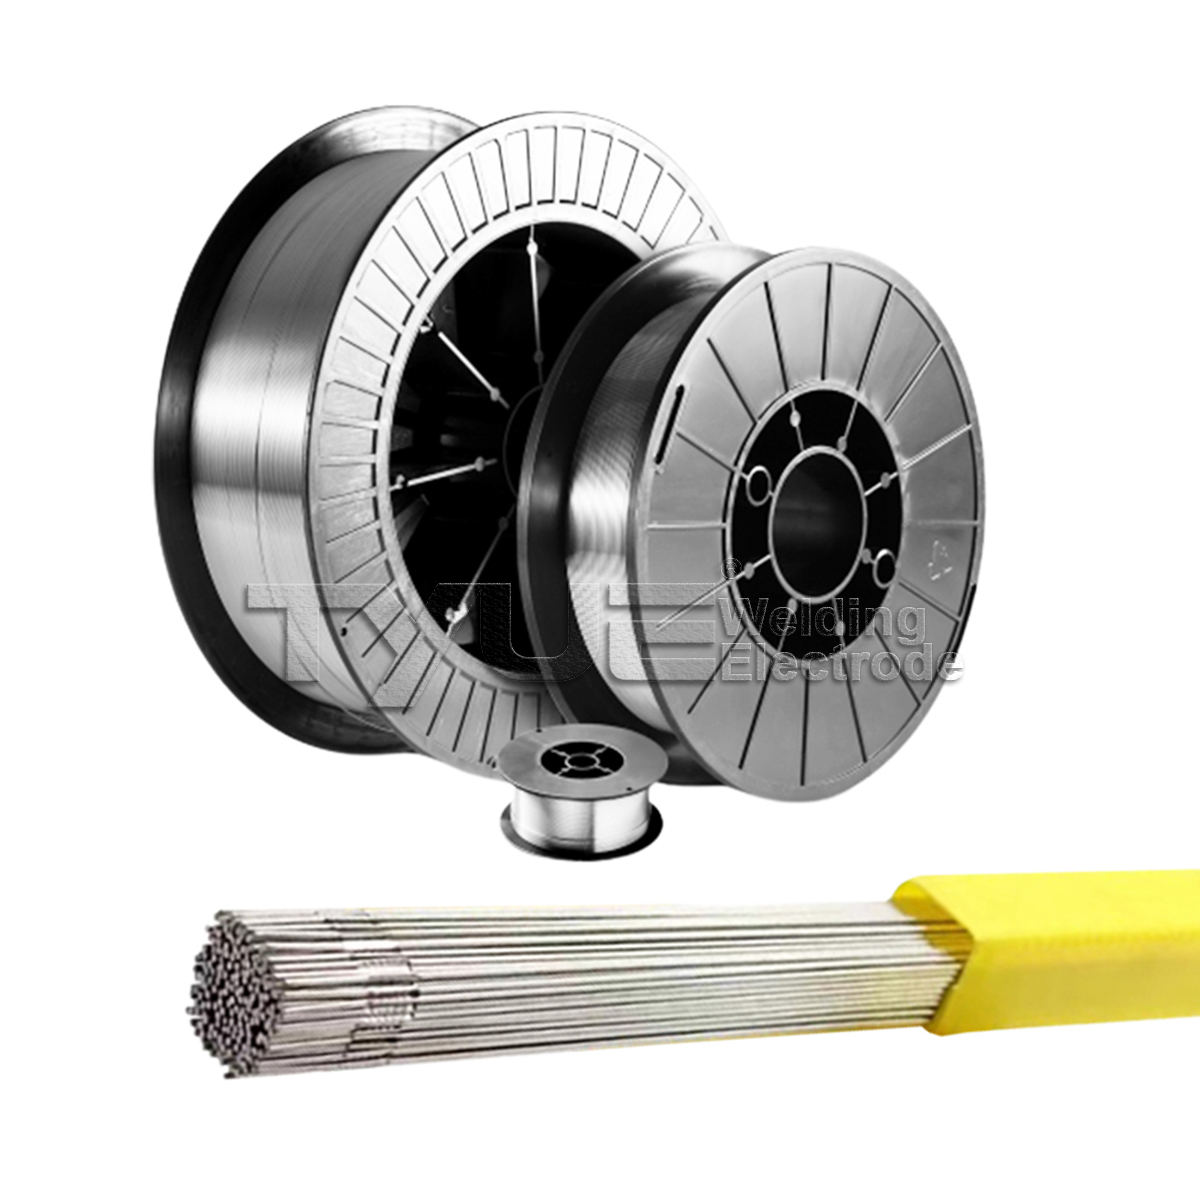
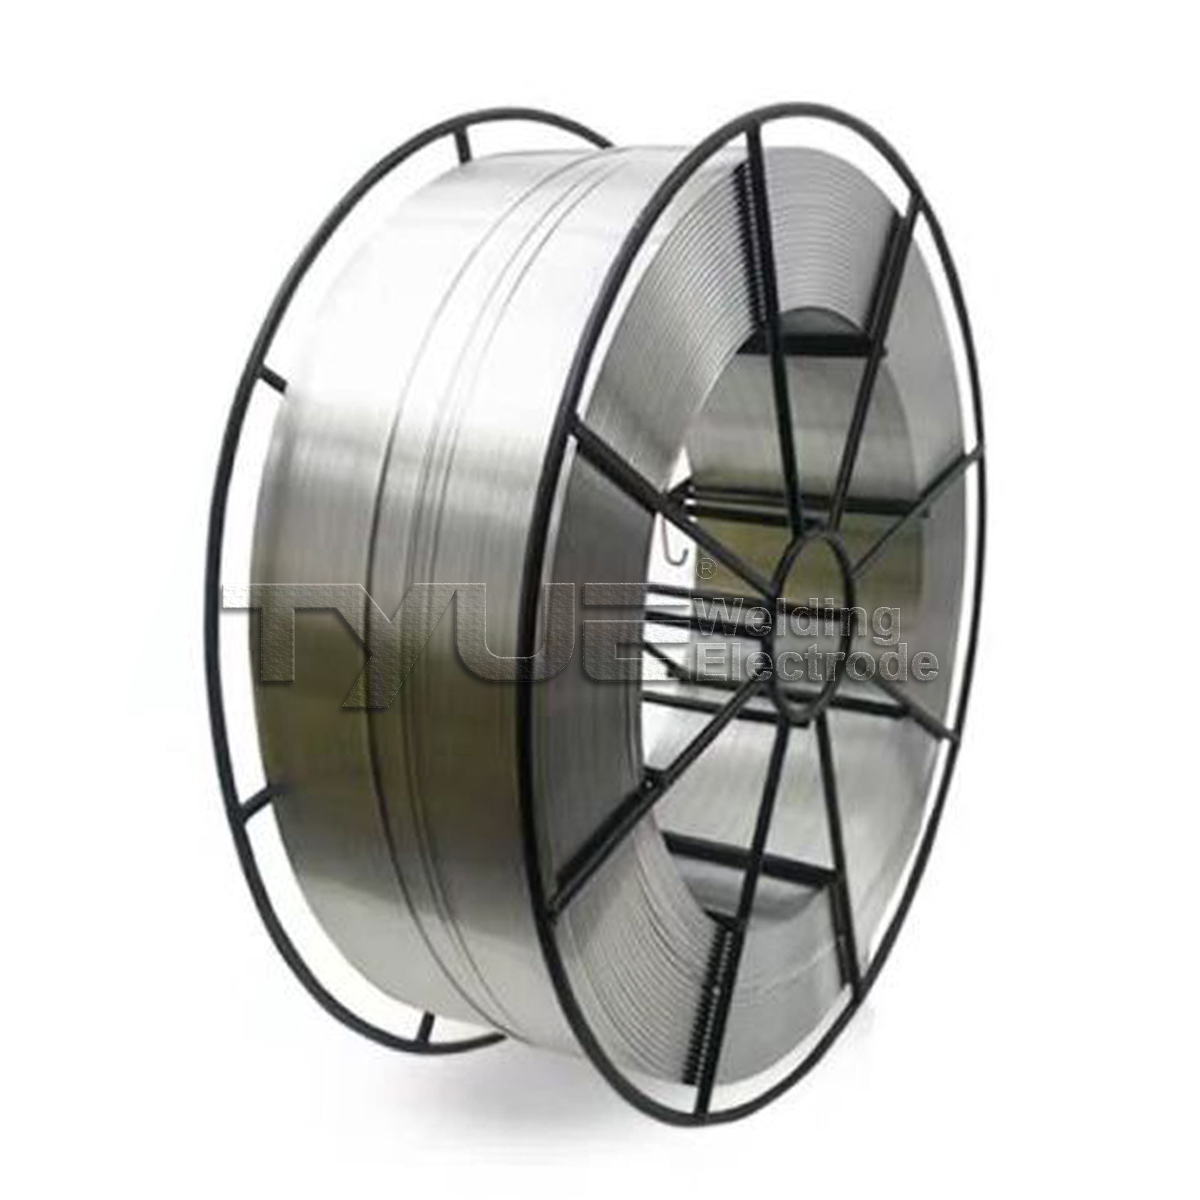
ER304 is an 18% Cr / 8% Ni austenitic stainless steel welding wire designed for GMAW (MIG) and GTAW (TIG) processes. It provides good general corrosion resistance and smooth weldability when joining matching base metals or similar 300-series stainless steels where niobium or titanium stabilization is not required.
2. Applications
-
Welding 304, 302, 301, and 308 base materials.
-
Fabrication of food processing equipment, brewery equipment, chemical tanks, sanitary piping, and architectural metalwork.
-
General utility stainless steel fabrication requiring modest temperature or mild chemical corrosion resistance.
3. Chemical Composition of Solid Wire (Wt %)
| Element | C | Si | Mn | P | S | Cr | Ni | Mo | Cu |
| Min. (%) | — | 0.30 | 1.00 | — | — | 18.0 | 8.0 | — | — |
| Max. (%) | 0.08 | 0.65 | 2.50 | 0.030 | 0.030 | 20.0 | 10.5 | 0.75 | 0.75 |
4. Typical Mechanical Properties of All-Weld Metal
- Ultimate Tensile Strength (UTS): 570 MPa (approx. 82.7 ksi)
- Elongation (L=4d): 38.0 %
5. Welding Parameters & Packaging (Reference)
- Shielding Gas (TIG): Argon
- Current Condition: DCEN (Direct Current Electrode Negative)
- Welding Positions: Horizontal, Flat, Vertical Up, Overhead (H, F, VU, OH)
- Standard Diameters: 1.6 mm, 2.0 mm, 2.4 mm, 3.2 mm (cut lengths of 1000 mm)
- Packaging: Typically supplied in 5 kg air-tight polyethylene bags inside plastic containers