

1. Description & Applications
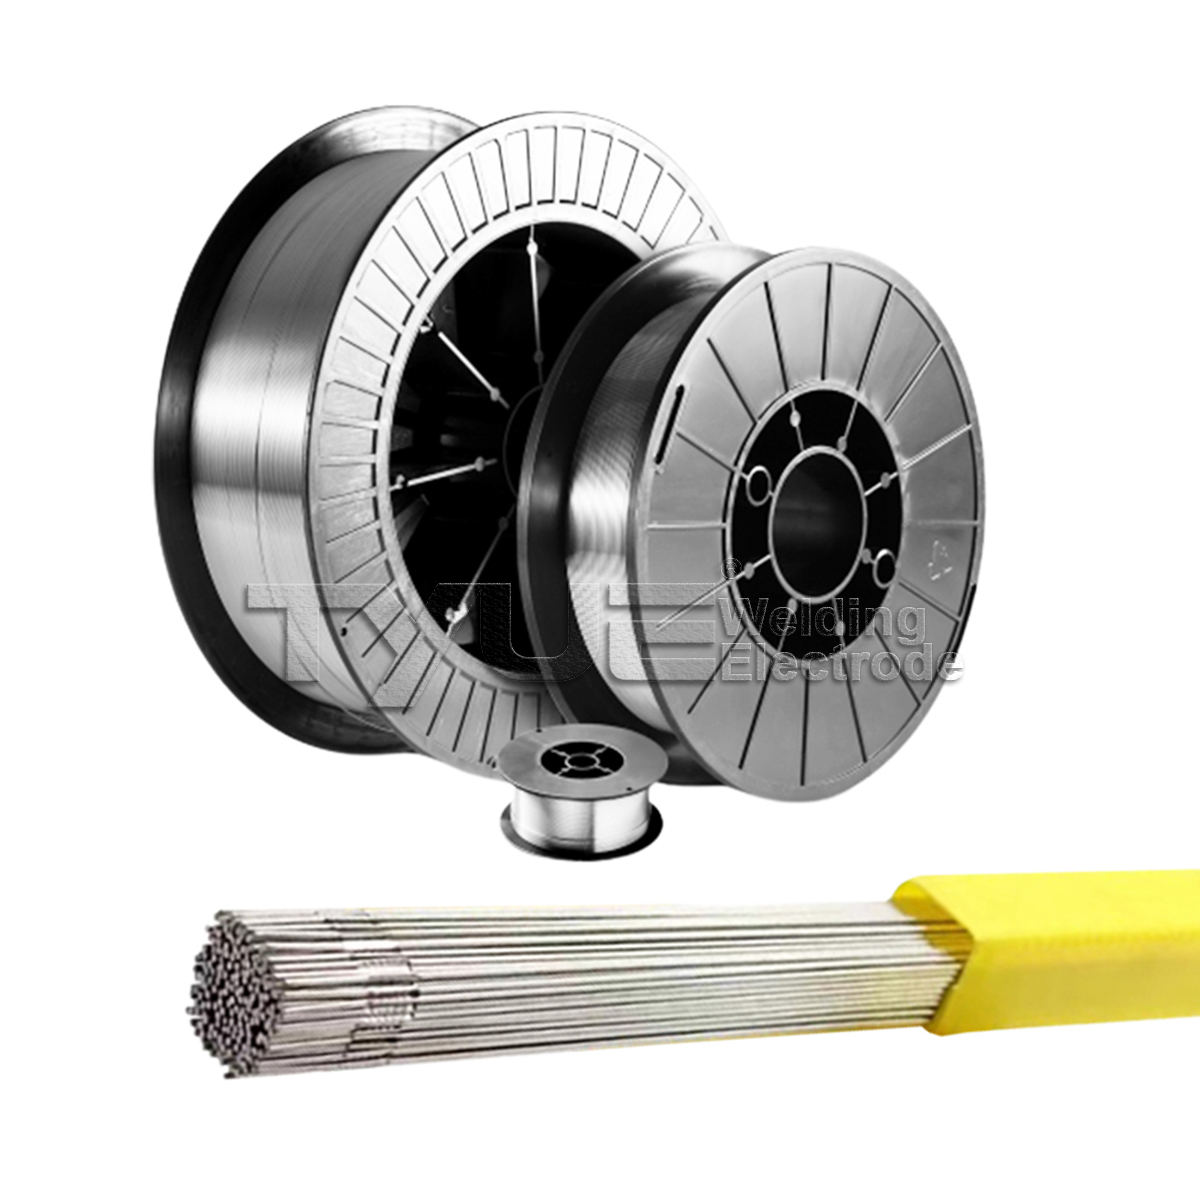
ER318 is a Niobium (Columbium) stabilized austenitic stainless steel solid welding consumable containing molybdenum. The inclusion of Niobium forms stable chromium/niobium carbides, preventing chromium carbide precipitation at grain boundaries during welding or elevated temperature service. This provides exceptional resistance to intergranular corrosion (weld decay).
2. Classification & International Standards
- AWS A5.9 / ASME SFA 5.9 ER318
- EN ISO 14343-A: W 19 12 3 Nb (TIG) / G 19 12 3 Nb (MIG) | W.Nr. / DIN 1.4576
- UNS NUMBER: UNS S31980
3. Chemical Composition (wt. %)
| C | Si | Mn | Cr | Ni | Mo | Nb |
|---|---|---|---|---|---|---|
| 0.04-0.05 | 0.4-0.8 | 1.5-1.7 | 18.9-19.5 | 11.5-12.0 | 2.6-2.8 | ≥12×C (approx. 0.5-0.7) |

4. Typical Mechanical Properties (As-Welded)
| Property | Typical Value |
|---|---|
| Yield Strength (Rp0.2) | 440-460 MPa |
| Tensile Strength (Rm) | 600-615 MPa |
| Elongation (A) | 35-42% |
| Impact Energy (20°C) | 70-100 J |
| Impact Energy (-60°C) | 70-90 J |
5. Storage & Handling Notes
- Store wire in a dry environment, protected from moisture. Reseal opened spools promptly.
- Control heat input (recommended ≤1.5 kJ/mm) and interpass temperature (recommended ≤150°C) to maintain corrosion resistance .-1
- Post-weld heat treatment is generally not required. For special service conditions, solution annealing at approximately 1050°C followed by water quenching may be considered.